

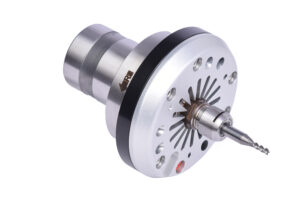

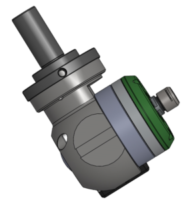


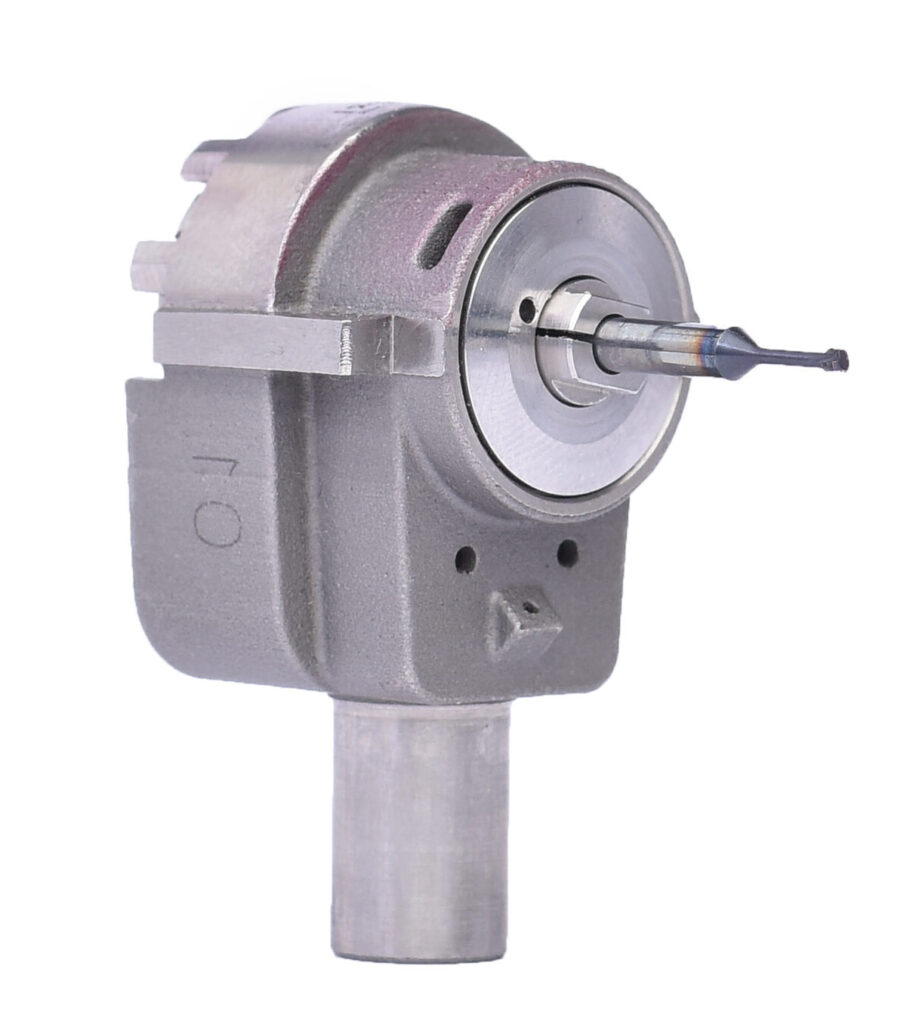











An energy, gas and oil customer was machining a gas turbine housing on an INTEGREX e-1060V/8 II. The operation was face ball-nose milling with a 1.5 mm cutter.
The problem
Long cycle time. Each part was taking 30 minutes on the machine spindle, and tool life was the other half of the problem — roughly one part per cutter. A 1.5 mm ball nose needs surface speed the machine cannot reach, so it was being run slowly and it was wearing out.
What changed
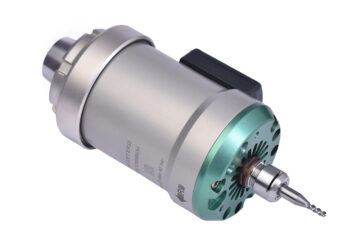
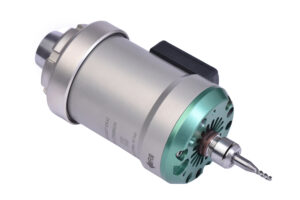
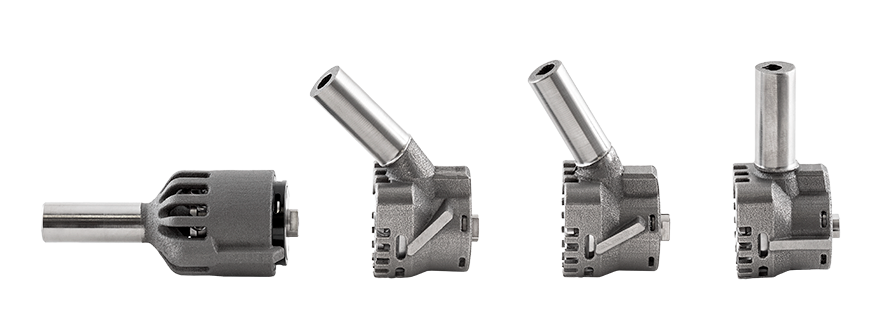
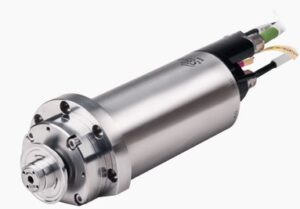
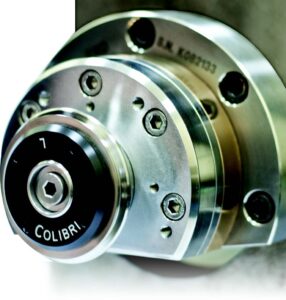
The HPC/POWER Jet Spindle was fitted for the operation. It is driven by the machine’s own high-pressure coolant, so there is no external power supply, no air line and no installation work — it loads and runs like any other tool holder.
The numbers
Same part, same machine, same operation. The only change is the spindle.
| Measure | Machine spindle | HPC/POWER Jet |
|---|---|---|
| Spindle Speed (rpm) | 3,000 | 22,000 |
| Cutting Speed (Vc in m/min) | 9.18 | 88.00 |
| Depth of Cut (mm) | 0.18 | 0.36 |
| Width of Cut (mm) | 0.975 | 1.281 |
| Table Feed (Vf in mm/min) | 1,013 | 7,665 |
| Machining Time (min) per part | 30 | 2 |
| Tool life – high, average, low | Low – 1 part per tool | High – 25 parts per tool |
| Surface Finish – high, average, low | Average | High |
| Metal Removal Rate (cm3/min) | 0.2753 | 4.154 |
Conditions
- Coolant pressure: 20 bar
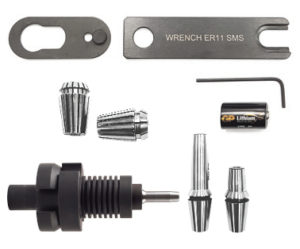
- Holder: ER11
- Material and hardness: A36, INO 316, 4140
- Cutting tool: EB-A2 015-012/06C4H45 702
- Tool diameter: 1.5 mm
- Number of teeth: 2
What it means
The result was a 93.4% reduction in cycle time, 28 minutes saved on every part, and $18.67 per part at a $40/hour machine rate. Tool life moved from one part per cutter to twenty-five.
The wider point is that the machine spindle was never the limit on this job — the tool was. A coolant-driven spindle speeder puts the rpm at the tool instead of asking the machine for it.
Read the full case study with every operating parameter or talk to us about your part.